


Vmc Cnc Milling Center
Dongguan Jide Precision Machinery Technology Co., Ltd. is one of the most credible manufacturers and suppliers of vmc cnc milling center in China. If you're going to wholesale high quality vmc cnc milling center made in China, welcome to get quotation and free sample from our factory. All customized products are with high quality and competitive price.
vmc cnc milling center features
1. The base parts of the machine tool base, column, spindle box, workbench and other basic parts all adopt high-strength lost foam casting molding technology to ensure the high stability of the basic parts. The casting structure has undergone machine tool dynamics analysis and finite element analysis to make its geometric structure more reasonable. The proper matching of the reinforcing ribs ensures the high rigidity of the foundation. The wide and solid machine bed, the design of full load support, and the structure conforms to the advanced design concept of material mechanics, which can ensure the heavy load capacity during processing.
2. High-speed and high-rigidity spindle unit combined with servo spindle motor; X/Y/Z adopts high-torque servo motor.
3. X/Y/Z adopts Taiwan high-precision and high-strength ball screw with special pair bearings for ball screw and high-precision imported locking.
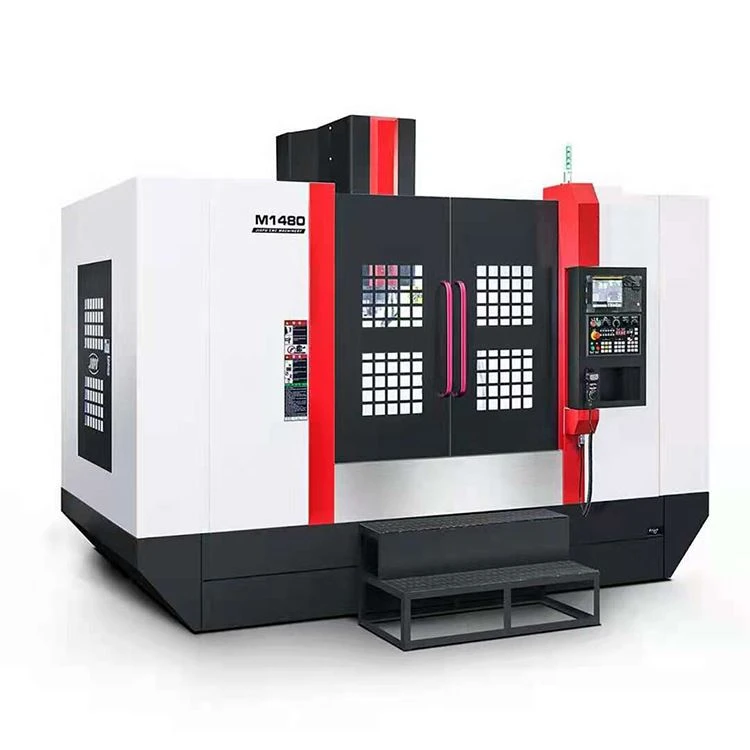

Parameters
CNC Machining center | 3 axis linear guideway | |||
Machine model | VMC1370 | |||
Quantity | 1pc | |||
Machine details | ||||
Item | Unit | Configuration | ||
System
| Operating system | Set | FANUC 0IMF β | |
Number of control servo axes | axis | 3 axis | ||
Work table
| Work table size | mm | 1300×700 | |
Max table load | kg | 1000 | ||
T-slot of worktable (number-size×spacing) | mm | 3-18×125 | ||
Travel
| Left and right stroke (X) | mm | 1200 | |
Back and forth stroke (Y) | mm | 700 | ||
Up and down stroke (Z) | mm | 700 | ||
Spindle
| Spindle taper hole (specification/installation size) | mm | BT40 | |
Spindle speed | rpm | 0-10000rpm | ||
Spindle drive mode | Belt type | |||
Distance from spindle center to column guide rail (suitable for vertical machines) | mm | 700 | ||
Distance from spindle end surface to table surface | mm | 190-640 | ||
Guideway
| X/Y/Z axis roller screw specifications | 3010/3010/3010 | ||
X-axis guide/line guide specification | Roller linear guideway | |||
Y-axis guide/line guide specification | Roller linear guideway | |||
Z-axis guide/line guide specification | Roller linear guideway | |||
Motor | X.Y.Z motor connection mode | Direct type | ||
Spindle motor parameters (power) | kw | 15 | ||
X.Y.Z axis motor parameters (power) | kw | 3/3/3 | ||
Spindle cooler capacity (gear type/750) | 250 | |||
Processing cooling pump power | w | 750W | ||
Feed
| X. Y. Z axis processing speed | m/min | 12/12/12 | |
X.Y.Z axis fast moving speed | m/min | 20/20/20 | ||
Power supply/air pressure
| Air source | kg/cm² | 6kg/cm² | |
Power requirement | kva | 30KVA | ||
Machine tool accuracy
| Positioning accuracy | mm | ±0.012/300 | |
Repeatability | mm | ±0.008/300 | ||
Machine specifications | Net weight of machine tool | T | 8.6T | |
Floor area of machine tool (length * width * height) | mm | 3800*3050*2900 | ||
Standard configurations
| Cutting water cooling system | 1 | ||
Processing blowing device | 1 | |||
Automatic lubrication device | 1 | |||
Work lights (explosion-proof) | 1 | |||
Action warning light | 1 | |||
Pre-sale teaching and after-sales service | 1 | |||
Electric box heat exchanger | 1 | |||
Spindle oil temperature cooler device | 1 | |||
Operation box storage box | 1 | |||
Hand-held electronic handwheel | 1 | |||
Full cover sheet metal | 1 | |||
Level adjustment block and bolt | 1 | |||
Tool box (hexagon socket/screwdriver) | 1 | |||
Vise | 1 | |||
Machine tool manual | 1 | |||
Main configurations | Origin | |||
Three-axis motor and servo | FANUC(Japan) | |||
Spindle motor and server | FANUC(Japan) | |||
Three-axis screw/line rail/guide rail | Taiwan HIWIN /Rexroth (Germany) | |||
24T disc tool magazine | Taiwan Sanjet /AIMACH BT40 tool magazine | |||
Spindle | TAIWAN KENTURN | |||
Electronic handwheel | NEDICON | |||
Bearing | NSK(Japan)/ FAG(Germany) | |||
Coupling | SG | |||
Unloading cylinder | HAOCHENG Taiwan | |||
Transmission belt | XUEFENG(Japan) | |||
Heat exchanger | Rucol(Taiwan) | |||
Processing cooling pump | ZHINENGHEYI | |||
Contactor | Schneider (France) | |||
Breaker | Schneider (France) | |||
Relay | Schneider (France) | |||
Switching power supply | MEANWELL (Taiwan) | |||
Central Lubrication System | Baotn | |||
Sheet metal | Special grade paint (domestic) | |||
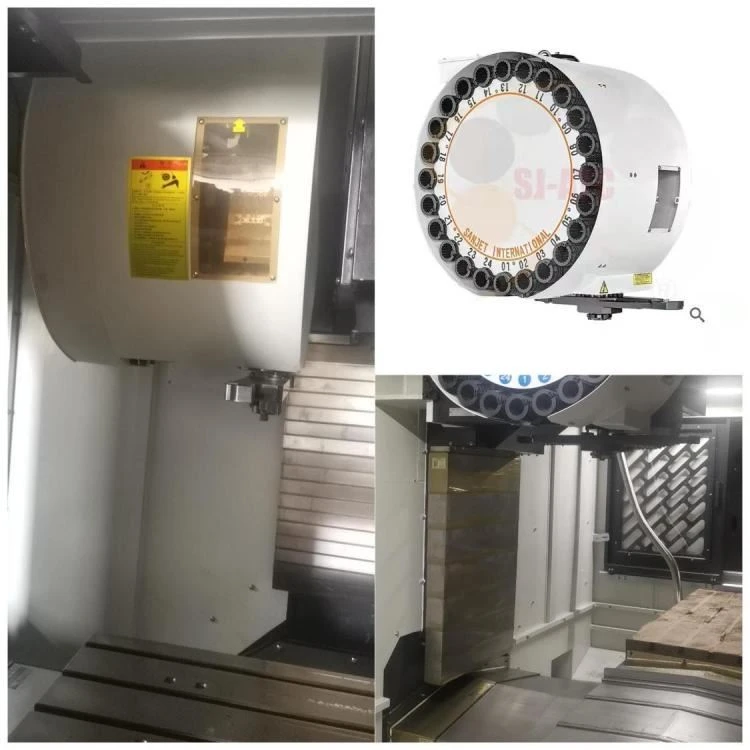

vmc milling center precision:
According to the national GB (JB/T8772.4-1998) standard. Note: The accuracy table of the assembly qualification certificate and the ballbar test accuracy report are attached.
Analysis of Nine Reasons for Unstable Workpiece Machining in Vmc Cnc Milling Center!
1. The scale of the workpiece is accurate, and the surface finish is poor
Causes of the fault: the tool tip is damaged and not sharp; the machine tool resonates and the placement is not stable; the machine tool is creeping; the processing technology is not good.
Solution: After the tool is worn or damaged, it is not sharp, then re-sharpening or selecting a better tool to re-calibrate; the machine tool resonates or is not placed smoothly, adjust the level, lay the foundation, and fix it smoothly; the cause of the mechanical creep is drag The plate guide rails are worn fiercely, and the balls of the lead screw are worn or loose. The machine tool should pay attention to maintenance. Clean the iron wire after work and add lubricating oil in time to reduce conflicts. Choose the coolant that is suitable for the workpiece to be processed. In this case, try to choose a higher spindle speed.
2. The phenomenon of taper and head size of the workpiece
The cause of the fault: the level of the machine is not adjusted properly, one high and one low, the placement is not stable; when turning the long axis, the dedicated data is relatively hard, the tool eats the knife deeper, resulting in a knife phenomenon; the tailstock thimble is not concentric with the spindle.
Solution: Use a spirit level to adjust the level of the machine tool, lay a thick foundation, and fix the machine tool to improve its resistance; select a reasonable process and appropriate cutting feed to prevent the tool from being forced to give it to the knife; adjust the tailstock.
3. The drive phase light is normal, and the size of the workpiece is large or small
The cause of the fault: the carriage of the machine tool runs at high speed for a long time, causing the screw and bearing to wear; the repeated positioning accuracy of the tool post has errors in the long-term use; the carriage can accurately return to the starting point of processing every time, but the size of the workpiece is still changed . This phenomenon is generally caused by the main shaft. The high-speed rolling of the main shaft causes severe wear of the bearing, leading to changes in processing dimensions. Metal processing WeChat, the content is good, worthy of attention.
Solution: Use a dial indicator to lean against the bottom of the tool post, and go through the system to modify a fixed cycle program, check the repeat positioning accuracy of the carriage, adjust the screw gap, and replace the bearing; use the dial indicator to check the repeat positioning accuracy of the tool post, Adjust the machine or replace the tool post; use the dial indicator to check whether the workpiece is accurately returned to the starting point of the program, if it can, check the spindle and replace the bearing.
4. The size of the workpiece is different from the actual size by a few millimeters, or a certain axis has been greatly changed
The cause of the fault: the rapid positioning speed is too fast, the drive and the motor can't respond; the mechanical carriage screw and the bearing are too tight and jammed after the long-term conflict and loss; the tool post is too loose after the tool is changed, and the lock is not tight; corrected The program is wrong, the head and tail are not responded to or the tool compensation is not cancelled; the electronic gear ratio or step angle of the system is set incorrectly.
Solution: If the rapid positioning speed is too fast, adjust the GO speed appropriately, cutting acceleration and deceleration and time to make the drive and motor work normally at the additional operating frequency; after the machine tool wears out, the carriage, screw and crane bearing are too tight If it is stuck, it is necessary to re-adjust and correct; if the tool holder is too loose after changing the tool, check whether the tool holder reversal is satisfied, check whether the worm gear inside the tool holder is worn, whether the gap is too large, whether the device is too loose, etc.; if it is If the program is caused by the cause, it is necessary to modify the program, improve according to the requirements of the workpiece drawing, select a reasonable processing technology, and write the correct program according to the instructions of the manual; if the scale error is found to be too large, check whether the system parameters are set properly, especially for electronics Whether the parameters such as gear and step angle are damaged, this phenomenon can be measured by using a dial indicator.
5. The processing arc function is not ambitious, and the scale is not in place
Fault reasons: resonance caused by the overlap of vibration frequency; processing technology; parameter setting is unreasonable, the feed speed is too high, so that the arc processing is out of step; the loosening caused by the screw rod gap or the out of step caused by the screw rod being too tight; the timing belt Wear.
Solution: Find out the resonant parts, change their frequency to prevent resonance; consider the processing technology of the workpiece data, and prepare the program reasonably; Regarding the stepper motor, the processing rate F cannot be set too large; whether the machine tool is sturdy, stable and dragged Whether the plate is too tight after being worn, the gap is enlarged or the tool holder is loose, etc.; replace the timing belt. Metal processing WeChat, the content is good, worthy of attention.
6. In mass production, the workpiece is out of tolerance occasionally
The cause of the fault: It is necessary to carefully check the tooling and fixtures, and take into account the operator's operation method and the reliability of the clamping. Because of the size changes caused by the clamping, it is necessary to improve the tooling to prevent the workers from making misjudgments due to human negligence; CNC The system may be affected by external power fluctuations or disturbances, and then actively generate disturbance pulses, which are transmitted to the drive and cause the drive to accept the remaining pulses to drive the motor to take away or reduce the phenomenon.
Solution: Understand and grasp its rules, try to choose some anti-interference methods, such as: blocking strong electric cables disturbed by strong electric fields and signal lines of weak electric signals, participating in anti-interference absorbing capacitance and shielding wire blocking, in addition, check the ground wire Whether the connection is strong, the grounding contact is the nearest, and all anti-interference methods are adopted to prevent the system from being disturbed.
7. The processing of a certain process of the workpiece is changed, and the scale of other processes is accurate
Fault reason: whether the parameters of the program segment are reasonable, whether they are in the reserved track, whether the programming pattern meets the requirements of the manual
Solution: If there are random teeth in the thread program segment, and the pitch is wrong, it immediately associates with the peripheral equipment (encoder) for processing the thread and the objective factors of the function.
8. Each process of the workpiece has the phenomenon of increasing or decreasing
Causes of faults: programming errors; unreasonable system parameter settings; improper equipment settings; mechanical transmission parts have regular and periodic changes
Solution: Check whether the instructions used by the program are performed in accordance with the requirements specified in the manual. It can be judged by dialing the dial indicator. Position the dial indicator at the beginning of the program and whether the carriage returns to the starting position after the program is completed, and then repeat the execution Even if the results are investigated, and the rules are grasped; check whether the system parameters are set reasonably or considered to be changed; whether the relevant machine tool equipment meets the requirements and whether the pulse equivalent is accurate in the connection calculation coupling parameters; check whether the transmission part of the machine tool is damaged, gears Whether the coupling is uniform, check whether there are periodic or regular problems, and if so, check the key parts and remove them.
9. The scale changes caused by the system are unstable
Fault reasons: unreasonable system parameter settings; unstable operating voltage; system is disturbed by the outside, causing the system to lose step; capacitance has been added, but the impedance between the system and the driver does not match, resulting in the loss of useful signals; signals between the system and the driver Transmission is abnormal; the system is damaged or internal problems.
Solution: Whether the speed, speed up time is too large, whether the spindle speed, cutting speed are reasonable, whether the parameter modification of the operator causes the system function to change; install a voltage stabilizing device; the grounding wire has been firmly connected, and the pulse output contact of the driver Add anti-disturbance absorption capacitors; select the appropriate capacitor model; check whether the signal connection between the system and the driver is shielded, whether the connection is secure, check whether the system pulse signal is lost or added; send the factory to repair or replace the motherboard.
Hot Tags: vmc cnc milling center, China, suppliers, manufacturers, factory, price, for sale, made in China, cnc milling turning, cnc milling carving production, cnc milling etching manufacturing, cnc milling drilling manufacturing, vertical cnc machining, Cnc Milling Machine Operation
Previous
Vmc Cnc CenterYou Might Also Like




Send Inquiry