


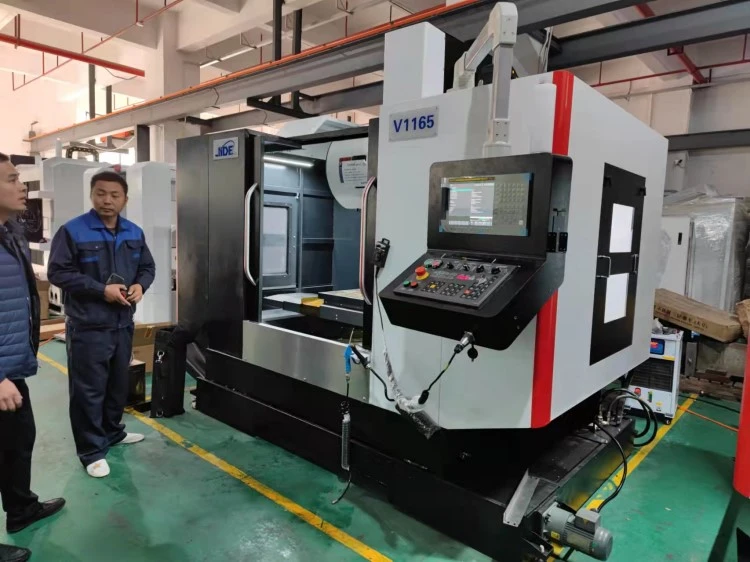
High Precision Milling Machine
workbench Work surface size mm 1000×600
Work table load g 800
Table T-slot (number-size ×spacing) mm 5- 18×100
travel Left and right stroke (X) mm 800
Front and rear travel (Y) mm 500
Up and down stroke (Z) mm 550
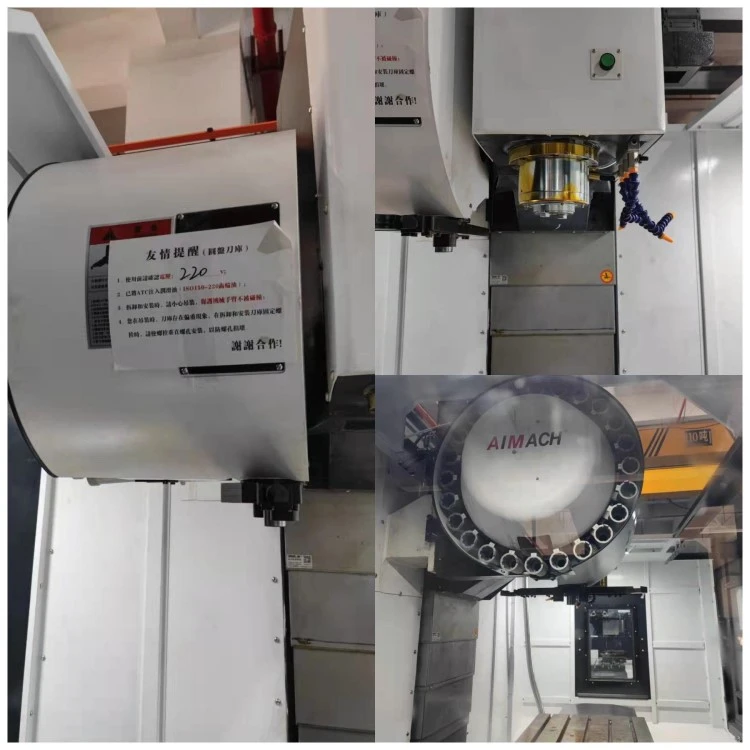
Dongguan Jide Precision Machinery Technology Co., Ltd. is one of the most credible manufacturers and suppliers of high precision milling machine in China. If you're going to wholesale high quality high precision milling machine made in China, welcome to get quotation and free sample from our factory. All customized products are with high quality and competitive price.
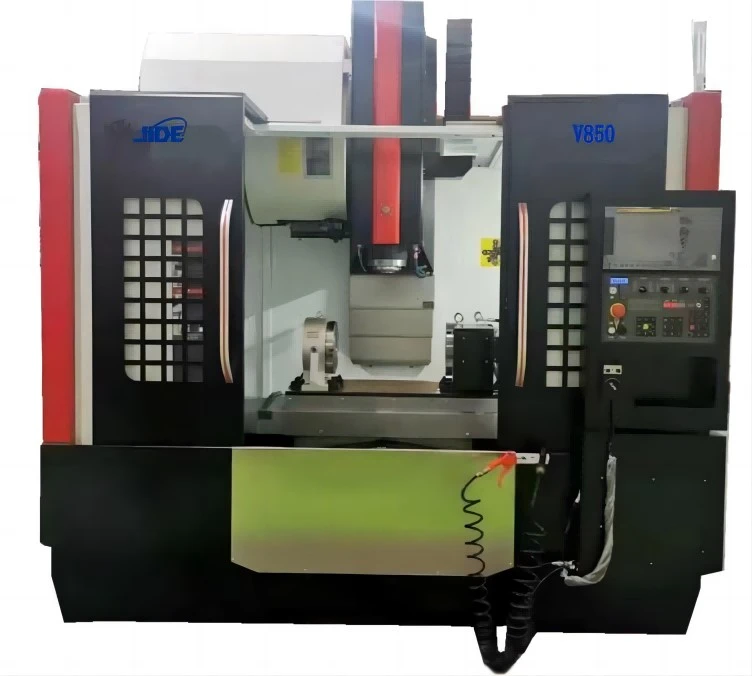
1. The main functions and characteristics of the company's machining center:
All high precision milling machines implement three-year warranty service (the gear is a wearing part with a one-year warranty), and the machine tool is maintained for life
v The appearance is beautiful and generous, and the overall layout is well-proportioned and coordinated.
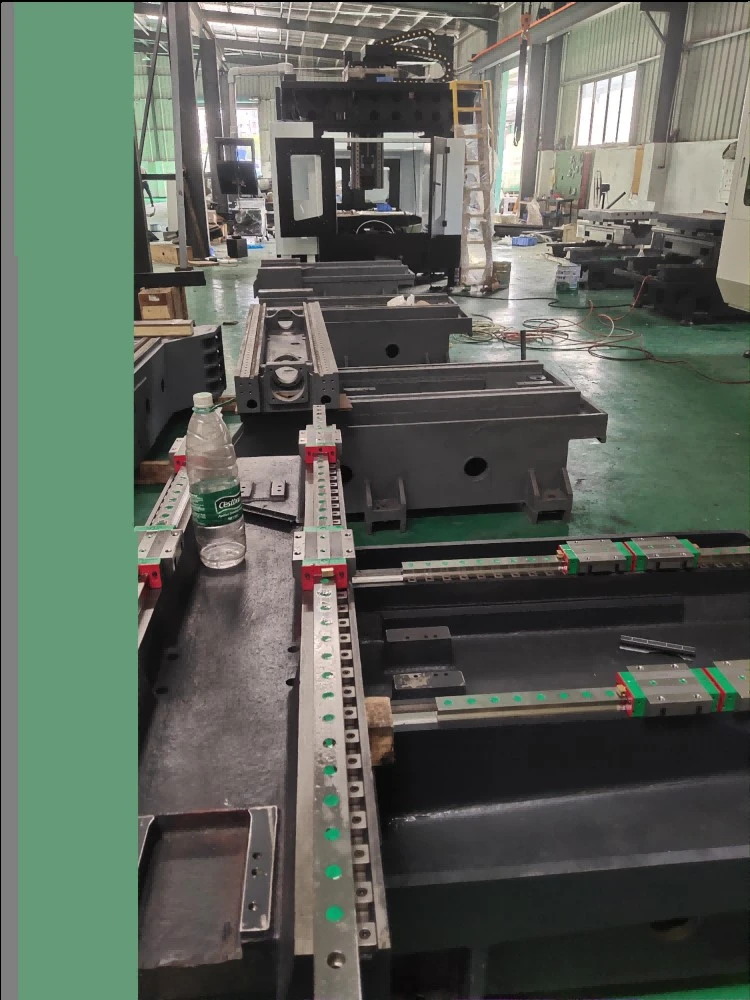
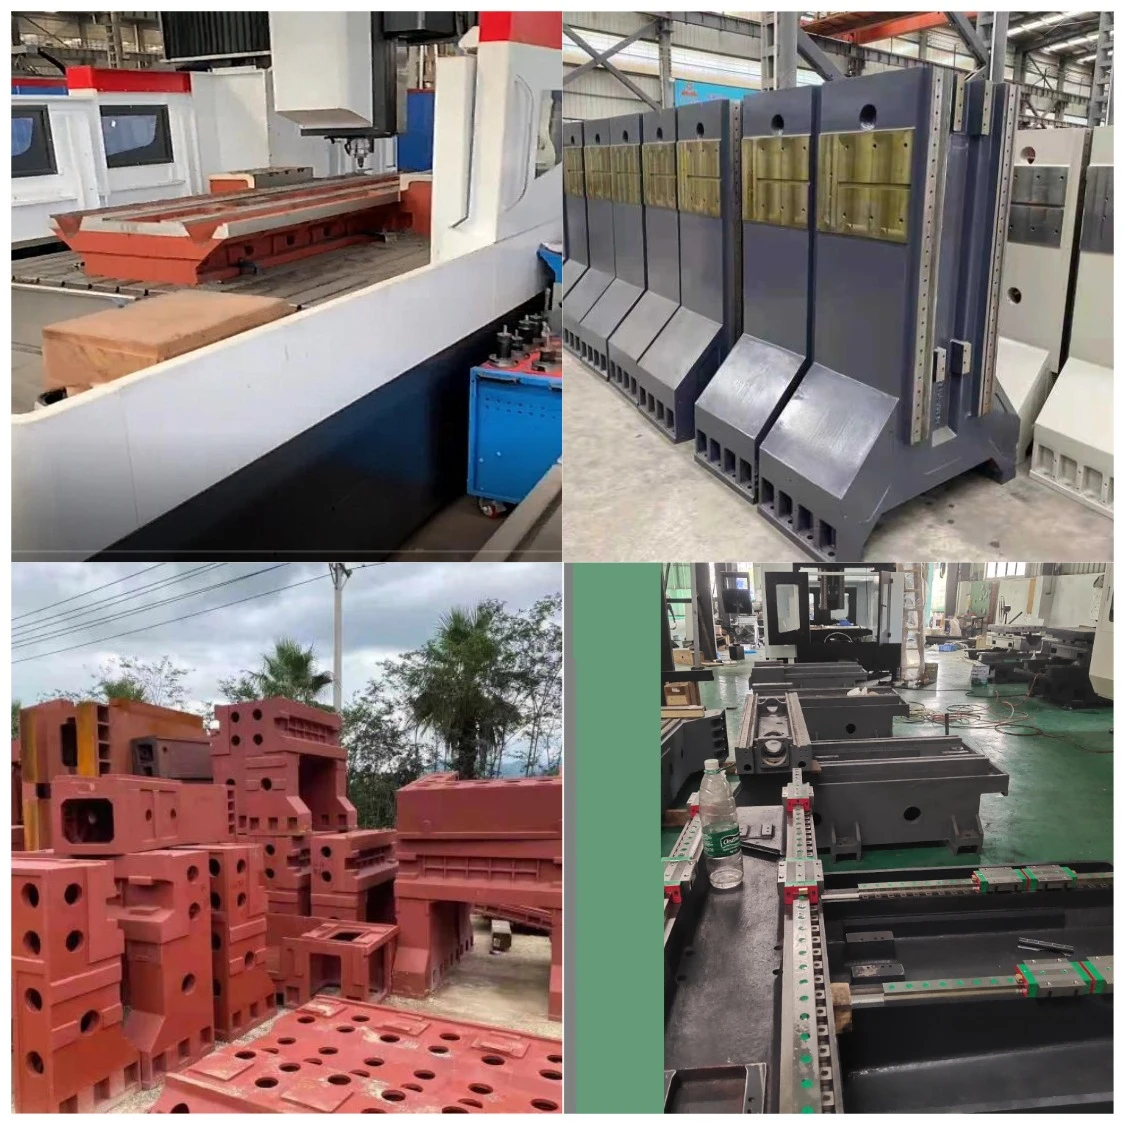
v Meehanite high-strength castings, high rigidity, high precision, long life
v The guide rail and workbench are quenched, tempered and hardened, precision researched
v The guide rail is pasted with Turcite-B high wear-resistant sheet, which is smooth and smooth.
v The guide rail is quenched by ultra-high frequency.
Machine parameter
|
Item |
Unit |
Parameter |
|
|
Control system |
Control system |
set |
MITSUBISHI M80B |
|
workbench |
Work surface size |
mm |
1000×600 |
|
|
Work table load |
|
800 |
|
|
Table T-slot (number-size ×spacing) |
mm |
5- 18×100 |
|
travel |
Left and right stroke (X) |
mm |
800 |
|
|
Front and rear travel (Y) |
mm |
500 |
|
|
Up and down stroke (Z) |
mm |
550 |
 g
|
Spindle |
Spindle taper hole (specification/installation size) |
mm |
BT40 |
|
Spindle maximum speed |
rpm |
0- 12000rpm |
|
|
Spindle transmission mode |
|
Direct |
|
|
Distance from spindle center to column guide |
mm |
500 |
|
|
Distance from spindle nose to work table |
mm |
150-780 |
|
|
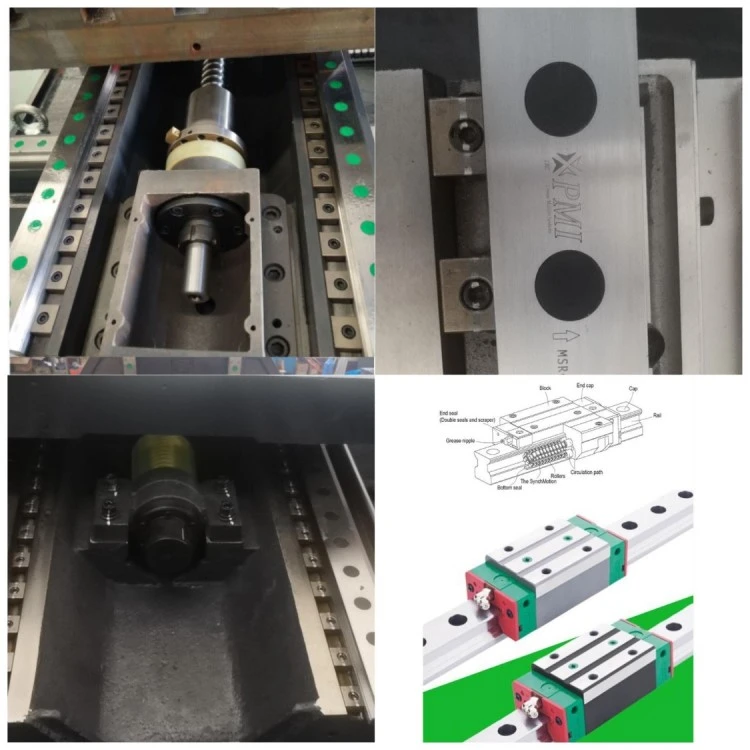
Linear guideway |
X/Y/Z axis ball screw specifications |
|
4012/4012/4012 |
|
X-axis guide/line rail specifications |
|
P-Class Sliding Roller Guideway 45 |
|
|
Y-axis guide/line rail specifications |
|
P-Class Sliding Roller Guideway 45 |
|
|
Z-axis guide/line rail specifications |
|
P-Class Sliding Roller Guideway 45 |
|
|
motor |
X.Y.Z motor connection |
|
Direct type |
|
Spindle motor parameters (power) |
|
11 |
|
|
X.Y.Z axis motor parameters (power ) |
|
3/3/3 |
|
|
Spindle Cooler Capacity (Gear/750) |
|
250 |
|
|
Machining Cooling Pump Horsepower |
w |
450W*2 |
|
|
feed |
X. Y. Z-axis machining speed |
mm/min |
18/ 18/ 18 |
|
X.Y.Z axis rapid traverse speed |
m/min |
36/36/36 |
|
|
Power / Air Pressure |
air source |
kg/cm² |
6kg/cm² |
|
power requirements |
|
20KVA |
|
|
Machine tool accuracy |
positioning accuracy |
mm |
±0.005/300 |
|
Repeatability |
mm |
±0.005/300 |
|
|
Machine Specifications |
Machine net weight approx. |
T |
5.5T |
|
Machine tool area (length*width*height) |
mm |
2900*2500*2550 |
|
|
|
|||
|
Standard accessories |
Cutting water cooling system |
1set |
|
|
Processing blower |
1set |
||
|
automatic lubricating device |
1set |
||
|
Work Lights (Explosion Proof) |
1set |
||
|
Action warning light |
1set |
||
|
Pre-sale teaching and after-sale service |
1set |
||
|
Electrical box heat exchanger |
1set |
||
|
Spindle oil temperature cooler |
1set |
||
|
Operation box storage box |
1set |
||
|
Handheld electronic handwheel |
1set |
||
|
Full cover plate |
1set |
||
|
Leveling blocks and bolts |
1set |
||
|
Tool box (hexagon socket/screw driver) |
1set |
||
|
Machine tool manual |
1set |
||
 w
 w
 va
The standard configuration
1>. MITSUBISHI M80B control system
2>. Direct spindle 12000 rpm
3>. Spindle oil cooler device
4>. Chip removal after flushing
5>. Automatic lubrication system
6>. Foundation screws and spacers
7>. Toolbox ( Phillips screwdriver, flat-blade screwdriver. Allen key, U disk inside with operating system electronic manual, 5m network cable, 2GB transmission memory card. )
8>. Working light (explosion proof light)
9>. Warning light
10>. Spindle blowing device
11>. Fully enclosed cover
12>. Automatic power off system
13>. Cooling water system
14>. Air Gun
15>. Rigid tapping function
16>. Electric box heat exchanger
17>. "Program Manual", "Operation Manual"/U disk information
Reasons and solutions for cracking or easy breakage of injection moulded products
Product cracking, including surface filiform cracks, microcracks, top whitening, cracking, and damage caused by part mucous membranes and flow channel mucous membranes. Cracking is divided into demoulding cracking and application cracking according to time. Cracks refer to the breakage of molded products when the mold is opened or ejected. Cracks sometimes occur when the product is brittle or poorly released from the mold. The speed at which the needle is ejected can also cause cracks, the faster the speed, the more prone to cracking.
The reasons for product cracking are roughly analyzed as follows:
1. Processing
① Excessive processing pressure, too fast speed, more filling materials, too long injection and pressure holding time will cause excessive internal stress and cracking.
②Rapid and strong drawing of products is easy to cause demoulding and cracking, so the speed and pressure of mold opening should be adjusted appropriately.
③ Properly increase the mold temperature to make the product easy to demould, and properly reduce the material temperature to prevent decomposition.
④Prevent cracking due to weld lines and plastic degradation resulting in lower mechanical strength.
⑤ Properly use the release agent, and pay attention to frequently remove the aerosol and other substances attached to the mold surface.
⑥ The residual stress of the product causes cracking. The internal stress can be eliminated and cracking can be prevented by annealing heat treatment immediately after the product is formed.
2. Mold aspect:
① Ejection must be balanced, such as the number and cross-sectional area of ejector pins must be sufficient, the demoulding slope must be sufficient, and the cavity surface must be smooth enough, so as to prevent cracking due to the concentration of ejection residual stress caused by external force.
②The structure of the product should not be too thin, and the transition part should adopt a circular arc transition as much as possible to avoid sharp corners and stress concentration caused by chamfering.
③ Minimize the use of metal inserts to prevent excessive internal stress caused by the difference in shrinkage between the insert and the product.
④The main channel is enough to make the gate material release from the mold in the future and when it is solidified, so it is easy to release from the mold.
⑤ For deep-bottom products, demoulding air holes should be properly set to prevent the formation of vacuum negative pressure.
⑥The sprue bushing and the nozzle joint should prevent the dragging of chilled hard material to make the product stick to the fixed mold.
3. Materials
①The content of recycled materials is too high, the product strength is too low, and it is easy to cause cracking.
② Excessive humidity will cause a chemical reaction between the plastic and water vapor, reducing the strength and causing ejection cracking. The molding temperature of each material should be observed, the residence time should be shortened to reduce resin decomposition and aging, and the drying conditions should be strengthened to inhibit hydrolysis. The degree of crystallization of the product can also be improved by increasing the mold temperature and prolonging the cooling time.
③The material itself is not suitable for the processing environment or the quality is not good, and it will cause cracking if it is polluted.
4. Machine aspect:
The plasticizing capacity of the injection molding machine should be appropriate. If it is too small, the plasticizing capacity will not be fully mixed and will become brittle. If it is too large, it will decompose.
It is also effective to use the following methods:
Slow down the mold opening speed and ejection speed to reduce the load on the molded product and reduce cracks.
Add fillets to the corners of molded products to prevent cracking.
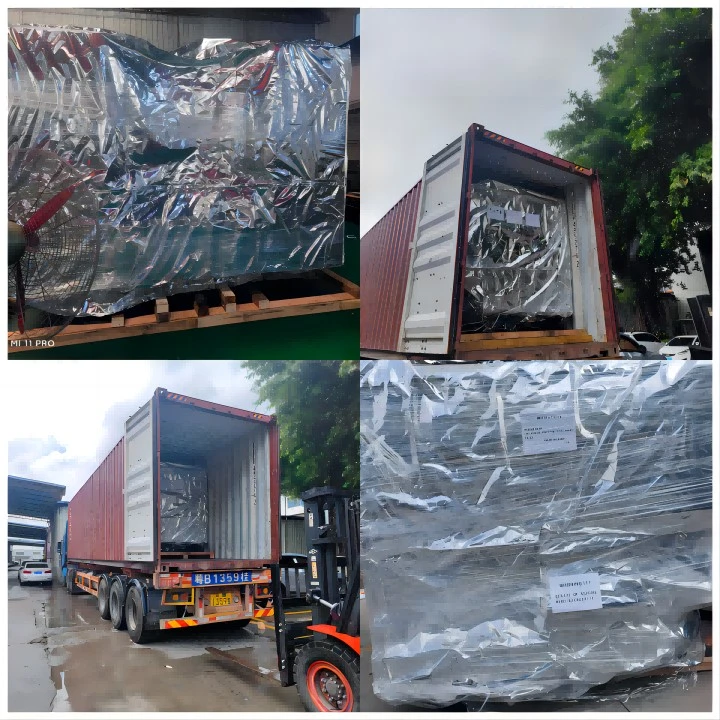
Packing and loading
Hot Tags: high precision milling machine, China, suppliers, manufacturers, factory, price, for sale, made in China, cnc machining market share, VMC Machining Center, cnc machining safety, cnc machining after sales service, 5 Axis Cnc Machine, High Speed Cnc Machining Center
You Might Also Like


Send Inquiry