


Machining Centre in Cnc V1165
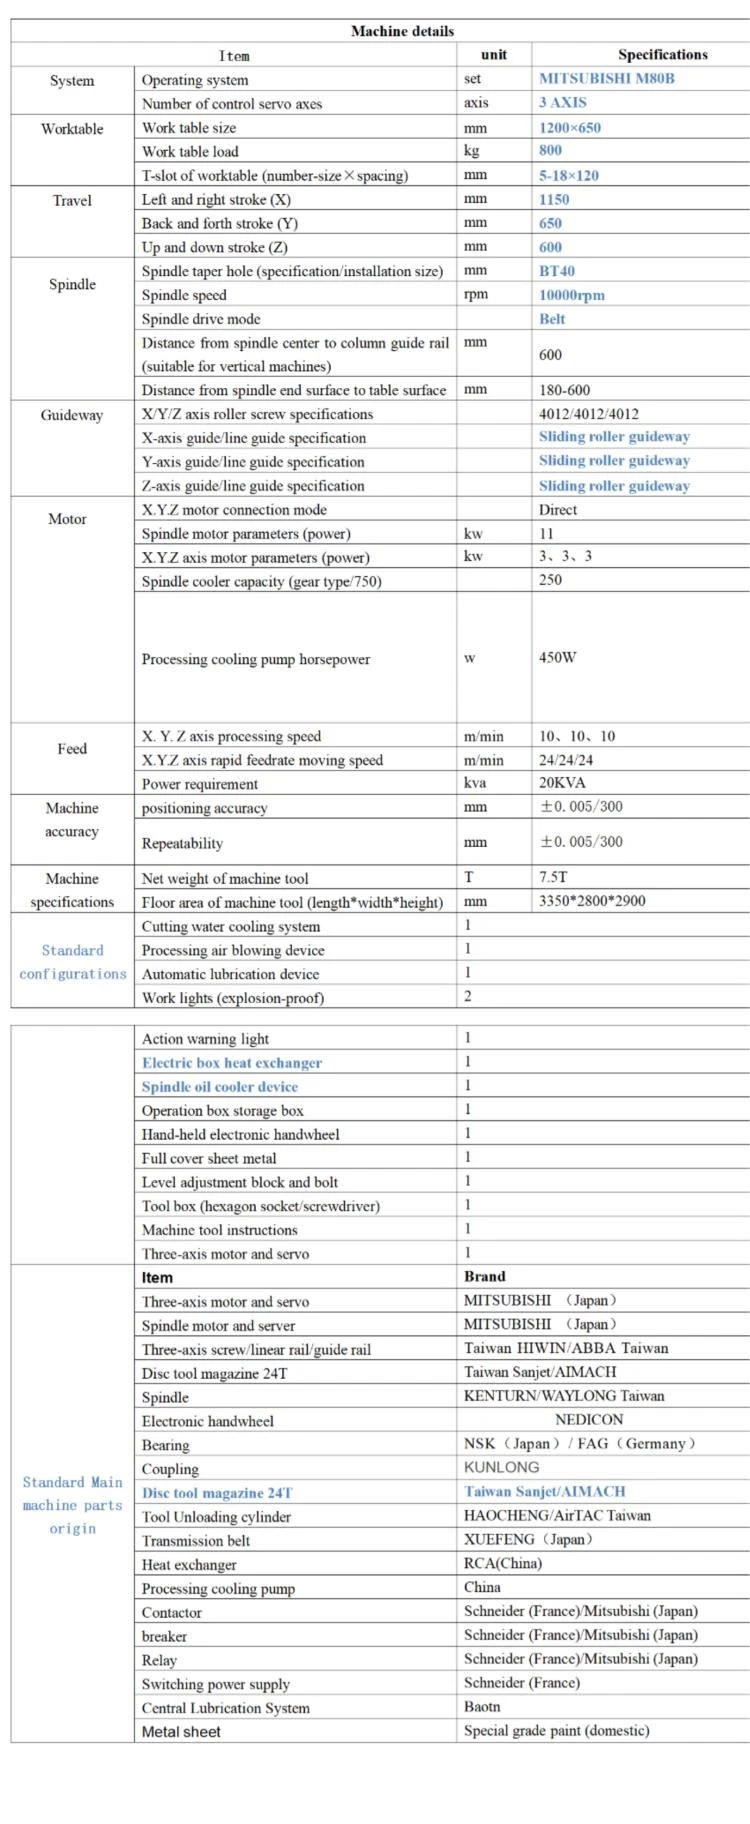
Number of control servo axes axis 3 axis
Work table size mm 1200×650
Max table load kg 800
T-slot of worktable (number-size×spacing) mm 5-18×120
Left and right stroke (X) mm 1150
Back and forth stroke (Y) mm 650
Up and down stroke (Z) mm 600
Spindle taper hole (specification/installation size) mm BT40
Spindle speed rpm 10000rpm
Spindle drive mode Belt type 7.5/11KW
Dongguan Jide Precision Machinery Technology Co., Ltd. is one of the most credible manufacturers and suppliers of machining centre in cnc v1165 in China. If you're going to wholesale high quality machining centre in cnc v1165 made in China, welcome to get quotation and free sample from our factory. All customized products are with high quality and competitive price.
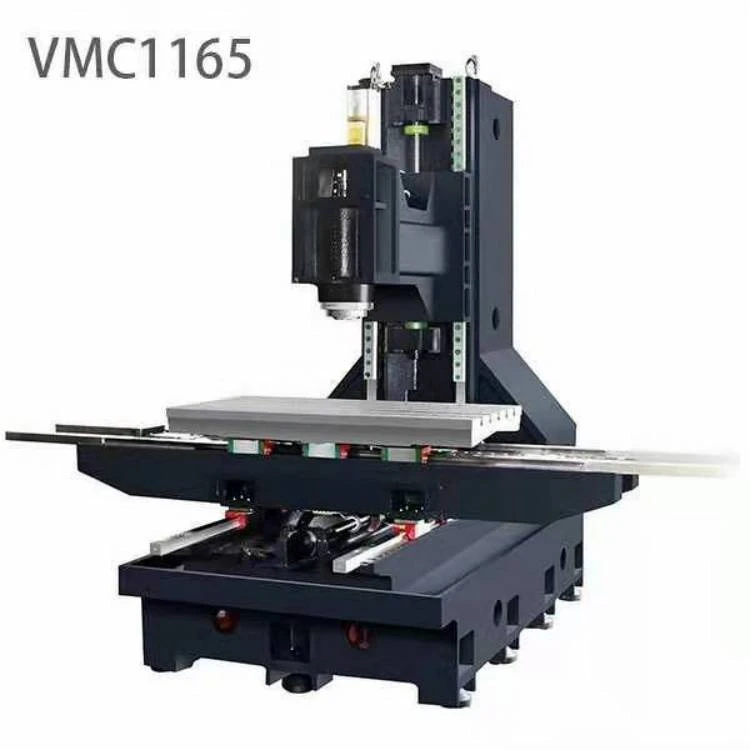 Detailed technical parameters pre-sales information of Machining centre in cnc V1165
Standard system: FANUC/SIEMENS/MITSUBISHI
Product Description:
1. X, Y, Z three-axis travel: 1100x650x600mm
2. The spindle rotation mode is belt connection, the maximum speed: 10,000 rpm.
3. The standard configuration of the tool magazine is a disc 24 tool magazine to meet the needs of customers.
4. The head unit is a heavy box structure with reinforced internal ribs and high rigidity.
5. The spindle tooling method adopts a hydraulic mechanism, the spindle is evenly stressed during tooling, and the life of the bearing is prolonged.
6. The electrical box adopts an internally divided and isolated design to separate the heating source of the controller. A heat exchanger is used to dissipate heat in the front to prevent external dust from entering the electrical box; a fan is used on the rear to dissipate heat from the fan hot plate.
7. The three-axis adopts high-precision ball screws, combined with precision nut pre-compression and end pre-tensioning devices, to ensure that the machine backlash and thermal deformation are kept at a low value for a long time.
8. X and Y axis adopt roller type linear guide, which has high rigidity, low noise, can make fast displacement and obtain cycle accuracy, and the fast moving speed is 36/36/24m/min.
9. All finished products have undergone laser positioning correction and circular testing to ensure positioning accuracy and servo characteristics, and strict inspection measures are taken before the machine is shipped to ensure the long-term stability of the machine's various accuracy.
Main parameters
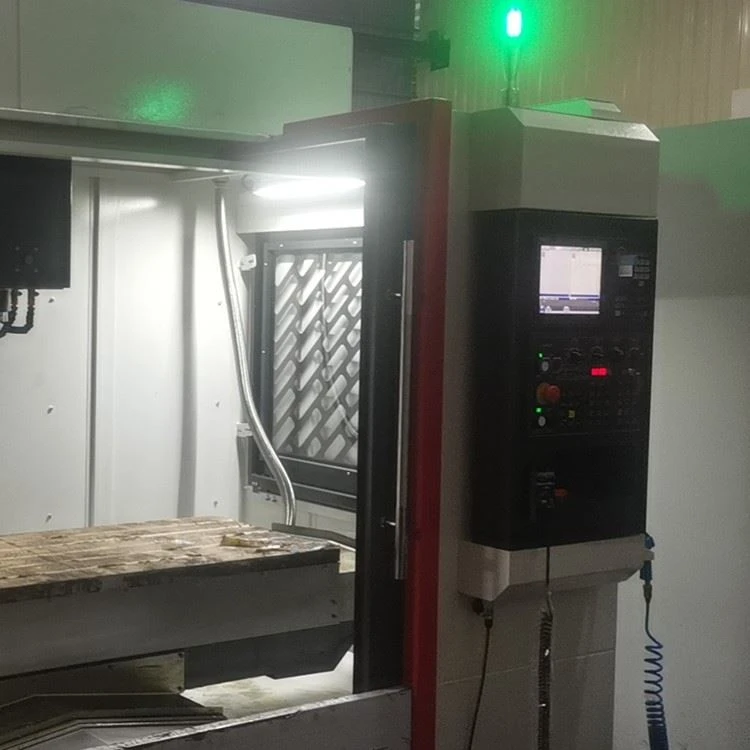
Z-axis 6 sliders blocks , table quenching, HIWIN C3 ball screw, HIWIN P4 roller linear guideway,
The oscillation defect of Machining centre in cnc V1165 generally occurs in the mechanical part and the feed servo system. There are many reasons for the oscillation. In addition to the inevitable transmission space, elastic deformation, frictional resistance and many other factors in the mechanical aspect, the influence of the relevant parameters of the servo system is also an important aspect. The servo system is divided into AC and DC. There are roughly four reasons for the servo system oscillation: a poor azimuth loop causes the output voltage to be unstable; b vibration caused by a bad speed loop; c servo system adjustable positioner is too large to cause voltage output distortion; d transmission machinery is installed as The gap between the screws is too large. Distortion of the output parameters of these control loops or too much open space for mechanical transmission equipment are the primary factors that cause oscillations. They can all be optimized through the servo control system.
How to eliminate oscillations:
1. Oscillation formed by the closed-loop servo system: Some CNC servo systems use semi-closed loop equipment, and the full-closed-loop servo system must adjust the parameters on the premise that part of the semi-closed loop system does not oscillate, so the two are completely different.
⒉Decrease the gain of the azimuth loop: there are standard values for reference in the servo system, for example, the FANUCO-C series is 3000, and the Siemens 3 system is 1666. If there is oscillation, the gain can be reduced appropriately, but not too much, because the steady state of the system must be ensured. fault.
3. Decrease the load inertia ratio: The load inertia ratio is generally set to 70% of the parameter shown when the oscillation occurs. If the defect cannot be eliminated, it is not advisable to continue to decrease the parameter value.
4. Participate in the proportional calculus (PID): the proportional calculus is a multi-function controller, which can not only effectively perform proportional gain on the current and voltage signals, but also can schedule the output signal to lag into the leading problem. Oscillation defects are sometimes caused by The output current and voltage lagging and leading occurs, then the PID can be used to schedule the output current and voltage phase.
5. Use high-frequency control function: The above discussion is about the parameter optimization method for low-frequency oscillation, and sometimes the CNC system will react due to some oscillations on the machine. The signal contains high-frequency harmonics, which makes the output torque unstable. , And then oscillates. Regarding this kind of high-frequency oscillation, a first-order low-pass filtering link can be added to the speed loop, which is a torque filter.
The speed command and the speed response signal are converted into a torque signal by the speed controller. The torque signal passes through a first-order filtering link to cut off the high frequency components, and then a useful torque control signal is obtained. After scheduling parameters, the frequency above 100 Hz generated by the machine can be cut off, and then the effect of eliminating high-frequency oscillation can be achieved. To sum up, the use of two-position reaction can make the system work in both full-closed loop and semi-closed loop methods, and then greatly improves the system's scheduling planning, and also increases the system's scheduling parameters. It can be seen from the time constant that the system can perform full-closed loop fault adjustment in discontinuous state and semi-closed loop adjustment in transitional state. Now take FANUCO-C as an example to briefly introduce the specific parameter adjustment process. First, set the parameter P8411# (DPFB) to 1, which is the function of selecting the two-sided response; P8499 is the larger amplitude of the azimuth response, generally set to 0; P8478 (numerator) and P8479 (denominator) are the constant settings for the middle conversion link , Can be set according to requirements; P8480 is the parameter setting code of the first-order delay link, and its setting plan is: 10~300mS, generally set to 100mS allocation; P8481 is the zero point height, generally 0, but it can be appropriate due to oscillation Turn it up a bit. The dual-position response function is a more flexible method of error correction, which has a good function of parameter optimization and system stability in the process of system debugging. The oscillation phenomenon of the machine tool system has become a common problem of the CNC full-closed loop system. When the system oscillates, the machine tool will have crawling and oscillation defects, especially in the horizontal axis with column and the axis of the rotating CNC table, the system exhibits a higher frequency of oscillation. This problem has become one of the important factors affecting the normal operation of CNC equipment.
FAQ :
What environmental protection requirements can your cable products meet?
We can design and manufacture machine that meet the environmental protection requirements of different regions .
I want a model that is different from others. Can you design it for me?
Yes, we can design a unique model based on your ID or by ourselves.
The product is too expensive, can you make it cheaper for me?
Yes, machine configurations at different prices will decide the machine price .according to your needs.like go for a more economic control system.
Hot Tags: machining centre in cnc v1165, China, suppliers, manufacturers, factory, price, for sale, made in China, Vertical Cnc, Vertical Machining Center 850, Vertical Machining Center Manufacturers, CNC Vertical Machining
You Might Also Like


Send Inquiry