


Double Spindle Cnc Lathe
Dongguan Jide Precision Machinery Technology Co., Ltd. is one of the most credible manufacturers and suppliers of double spindle cnc lathe in China. If you're going to wholesale high quality double spindle cnc lathe made in China, welcome to get quotation and free sample from our factory. All customized products are with high quality and competitive price.
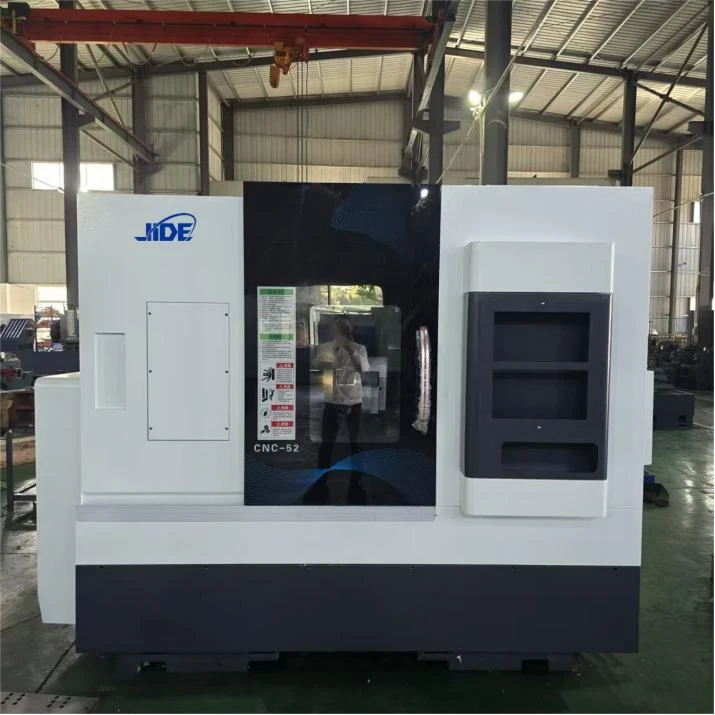
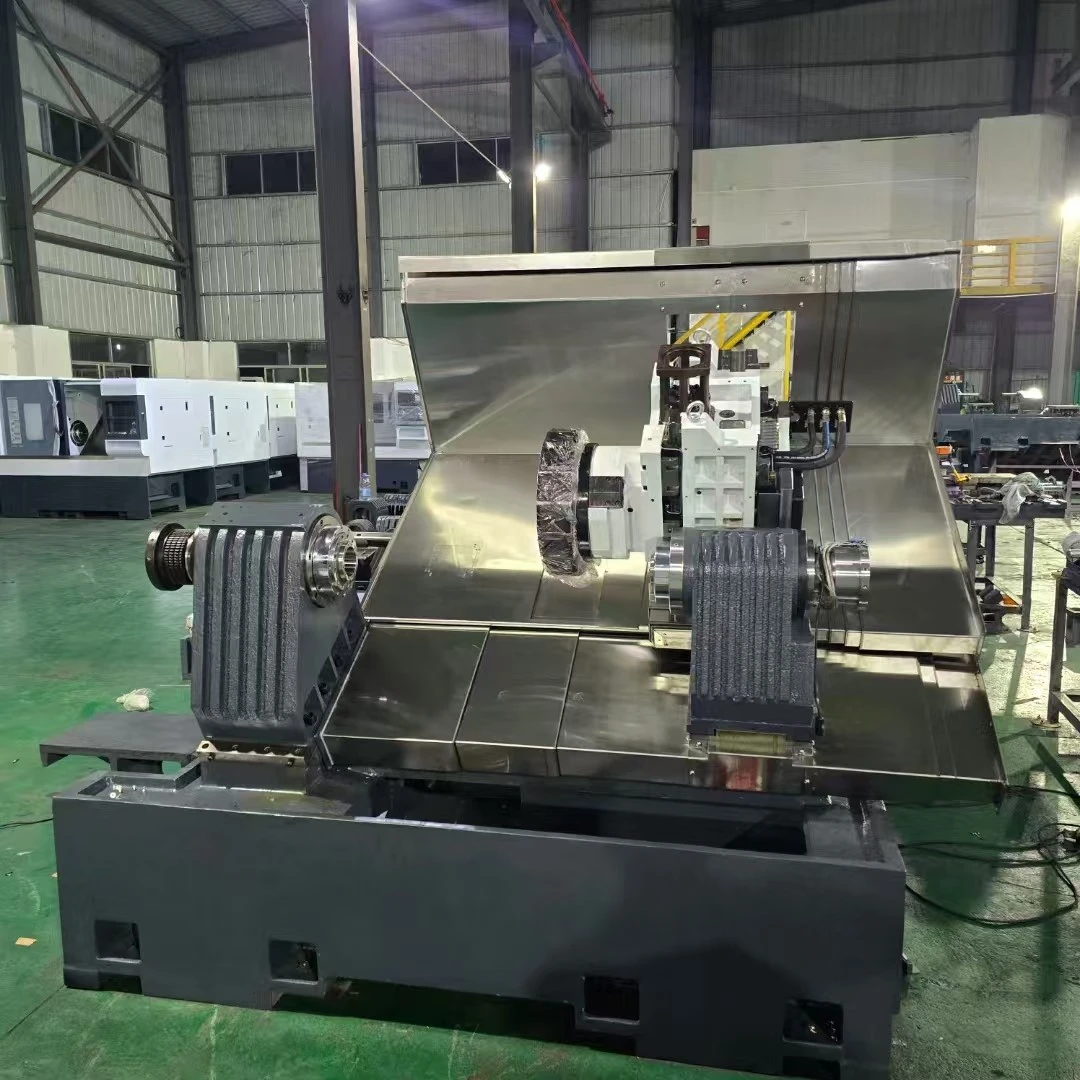
With the continuous development of mechanical manufacturing technology, the structure of parts is becoming more and more complex, and the requirements for processing accuracy are becoming higher and higher. Multiple changes in the processing process not only make the processing quality of parts unguaranteed, but also greatly reduce the processing efficiency due to multiple workpiece installation and tool setting processes. Double spindle CNC lathe can complete all processing of workpieces that require multiple processing steps in one clamping, which not only reduces the processing errors caused by multiple clamping, but also improves the processing efficiency. It can well meet the production requirements of modern enterprises, especially in the fields of aviation and aerospace. The efficient application of double spindle turning centers plays a decisive role. However, due to the complex and diverse structure and motion forms of this type of machine tool, there are problems such as difficulty in CNC program writing and correctness detection in actual applications. These problems restrict the efficient application of turning centers and bring difficulties to enterprises in rapid production [1]. Using virtual simulation technology, taking the actual machine tool as the prototype, a simulation processing system of the machine tool is constructed in the virtual simulation platform, so that it has the processing function that is completely consistent with the actual machine tool, and the workpiece is processed by virtual simulation. This method can quickly complete the virtual processing of workpieces without consuming production resources, verify the correctness of the CNC program, and predict the quality problems that exist in the processing process, providing reliable protection for the safety and efficiency of machine tools in the actual processing process.
|
Machine model |
Parameter |
Unit |
|
Maximum swing diameter over bed |
520 |
㎜ |
|
Maximum machining diameter on pallet |
360 |
㎜ |
|
Maximum machining length |
450 |
㎜ |
|
Spindle speed range |
100~4000 |
rpm |
|
Main motor power |
11/15KW |
KW |
|
Sub-spindle turning range |
0/4000 |
rpm |
|
Sub-spindle motor power |
8.8/11KW |
KW |
|
C2 live tool power |
3/3.7 |
KW |
|
C2 live tool speed |
3000/4000 |
rpm |
|
Maximum number of tools on tool holder |
15 |
T |
|
X-axis travel |
210 |
㎜ |
|
Z-axis travel |
610 |
mm |
|
Y-axis travel |
+50,-50 |
mm |
|
Z2 sub-spindle travel |
600 |
mm |
|
X-axis/Z-axis minimum movement |
0.001/0.001 |
㎜ |
|
X-axis/Z-axis rapid traverse speed |
24/24 |
m/min |
|
Spindle C-axis indexing |
0/360 |
° |
|
Sub-spindle C-axis indexing |
0/360 |
° |
|
Tool loading method |
BMT45-15-Y turret |
set |
|
Total tailstock travel (double spindle distance) |
610 |
mm |
|
X-axis/Z-axis repeatability |
≤0.003/0.005 |
㎜ |
|
Surface roughness |
≤0.63 |
um |
|
Spindle bore diameter |
Φ66 |
㎜ |
|
Bar hole diameter |
Φ52 |
㎜ |
|
Sub-spindle bore diameter |
Φ56 |
mm |
|
Sub-spindle bar diameter |
Φ42 |
mm |
|
Bed slope angle |
30 |
|
|
Overall dimensions (length x width x height) |
3500*2100*2000 |
㎜ |
|
Machine net weight |
4100 |
kg |
Machine Tool Structure Analysis JD-460M dual-spindle turning center is equipped with a turret with X, Y, and Z1 motion axes, the main spindle has C1 rotation axis function, and the sub-spindle has two motion axes Z2 and C2. As shown in Figure 2, the working surface of the bed is a high-rigidity 45° easy-chip removal inclined structure, on which the main spindle, sub-spindle and saddle sliding along the bed are installed, in which the main spindle is fixed to the bed, the sub-spindle sliding along the bed is axially opposite to the main spindle, and the servo power tool holder is fixed on the slide sliding along the X-axis direction of the saddle.

1. Spindle 2. Sub-spindle 3. Bed 4. Saddle 5. Slide 6. Tool holder

3. Simulation Processing 3.1 NC Program Generation The dual-spindle turning center has powerful processing functions, but the workpiece structure is usually complex. It is difficult to implement NC programming for complex workpieces by manual programming. The geometric model of the part is established in UG and other three-dimensional software, and the advanced CNC processing function in UG is used to process the workpiece and generate the correct tool path file. However, this file cannot be directly recognized by the CNC machine tool, so it needs to be post-processed. The post-processing module in UG can post-process the tool path files of three axes and below to generate NC programs that can be directly recognized by the machine tool, but it is powerless for complex files above three axes [4]. In view of the structural characteristics of the dual-spindle turning center, a special post-processor MAXX-POST is developed using the UG post-processing module. This post-processor can specifically process the pre-processing tool path files of the workpiece suitable for the dual-spindle turning center, and produce NC programs that can be directly recognized by the machine tool to meet the processing needs.
3.2 Virtual simulation processing and verification Add the NC program generated in UG to the virtual simulation system, add the models of the blank and workpiece to the system, set the G code offset (i.e. machining tool setting), and then perform simulation processing, as shown in Figure 5. In simulation processing, it is necessary not only to observe whether the status of the tool and the workpiece is reasonable, but also to analyze and deal with the existing problems according to the warning content to ensure the correctness of the pre-process and NC program.
4. Actual verification After virtual simulation processing, after verifying the correctness of the NC program, the machining workpiece is verified by example. Load the NC program that has been verified by virtual simulation into the actual machining machine tool and perform actual machining on the workpiece. The tool path of the tool during machining is consistent with the simulation machining, and there are no interference, collision and other problems.
|
Item |
Model |
Brand |
Qt |
|
|
Spindle (with C-axis + brake disc) |
A2-6 |
Taiwan HUACHUANG |
1 |
|
|
Sub-spindle (with C-axis indexing) |
A2-5 |
HUACHUANG |
1 |
|
|
Spindle motor servo |
11/15KW |
Japan Fanuc |
1 |
|
|
Spindle motor power |
11/15KW |
Japan Fanuc |
1 |
|
|
Sub-spindle motor servo |
11KW |
Japan Fanuc |
1 |
|
|
Sub-spindle motor power |
8.8/11KW |
Taiwan Huachuang |
1 |
|
|
X-axis servo motor torque |
12nm |
Japan Fanuc |
1 |
|
|
X-axis servo motor power |
2KW(brake) |
Japan Fanuc |
1 |
|
|
Z-axis servo motor torque |
12nm |
Japan Fanuc |
1 |
|
|
Z-axis servo motor power |
2KW |
Japan Fanuc |
1 |
|
|
Y-axis servo motor torque |
8nm |
Japan Fanuc |
1 |
|
|
Y-axis servo motor power |
1KW(brake) |
Japan Fanuc |
1 |
|
|
Z2-axis servo motor torque |
8nm |
Japan Fanuc |
1 |
|
|
Z2-axis servo motor power |
1KW(brake) |
Japan Fanuc |
1 |
|
|
C2 live tool servo motor torque |
28NM |
Japan Fanuc |
1 |
|
|
C2 live tool servo motor power |
3/3.7KW |
Japan Fanuc |
1 |
|
|
Linear guide (X-axis) |
35(roller) |
Taiwan Hiwin/PMI |
2 |
|
|
Linear guide (Z-axis) |
35(roller) |
Taiwan Hiwin/PMI |
2 |
|
|
Linear guide (Z2-axis) |
35(roller) |
Taiwan Hiwin/PMI |
2 |
|
|
Ball screw (X-axis) |
32 /10 |
Taiwan Hiwin/PMI |
1 |
|
|
Ball screw (Z-axis) |
40/10 |
Taiwan Hiwin/PMI |
1 |
|
|
Ball screw (Z2-axis) |
32 /10 |
Japan Fanuc |
1 |
|
|
Fanuc system |
OI-TF(3package) |
Taiwan AUTOSTRONG |
1 |
|
|
Rotary cylinder (hollow) |
8 inch |
Taiwan Hiwin/PMI |
1 |
|
|
Hydraulic chuck (hollow) |
8 inch |
Taiwan AUTOSTRONG |
1 |
|
|
Sub-spindle cylinder (hollow) |
6 inch |
Taiwan AUTOSTRONG |
1 |
|
|
Sub-spindle chuck (hollow) |
6 inch |
Taiwan AUTOSTRONG |
1 |
|
|
Hydraulic station |
40L/60L |
Made in Guangdong, China |
1 |
|
|
Servo (live tool) turret |
100 center height 15T |
LIANQI /SWIFT, Taiwan |
1 |
|
|
Live tool seat |
BMT45(ER25) |
LIANQI /SWIFT |
1 |
|
|
Live tool collet |
ER32(round hole 32/40) |
LIANQI /SWIFT |
1 |
|
|
External cylindrical tool holder |
Φ32 |
Turret with |
1 |
|
|
Face tool holder |
25/25 |
Turret with |
1 |
|
|
Press block |
25X25 |
Turret with |
8 |
|
|
Machine tool base |
Integral casting |
domestic |
1 |
|
|
Hydraulic sub-spindle tailstock |
Split casting |
domestic |
1 |
|
|
Sheet metal cover |
domestic |
1 |
||
|
Internal protection |
|
Full guard protection |
1 |
|
|
Live tool 90 degrees |
BMT-45(ER25)90° |
LIANQI /SWIFT, Taiwan |
1 |
|
|
Live tool 0 degrees |
BMT-45(ER25)0° |
LIANQI /SWIFT, Taiwan |
1 |
The general method of establishing a virtual simulation processing system for machine tools in Double spindle cnc lathe is introduced, and the virtual simulation processing system is established with a double spindle turning center as the object. A rotating part is used as a processing sample, and virtual simulation processing is performed on it to verify the correctness of the NC program, and the sample is actually processed. The results show that the virtual simulation processing system can accurately verify the correctness of the NC program, and correctly predict the possible interference, collision and other dangerous situations that may occur during processing, which can effectively ensure the safety and efficiency of machine tool use.


Hot Tags: double spindle cnc lathe, China, suppliers, manufacturers, factory, price, for sale, made in China, cnc horizontal machine, cnc lathe tailstock, cnc centre lathe, Horizontal Cnc Lathe Machine, Cnc Turning Machine With FANUC Control, Cnc Lathe Machine Slant Bed With Turret
Previous
CNC Gang LatheYou Might Also Like


Send Inquiry