

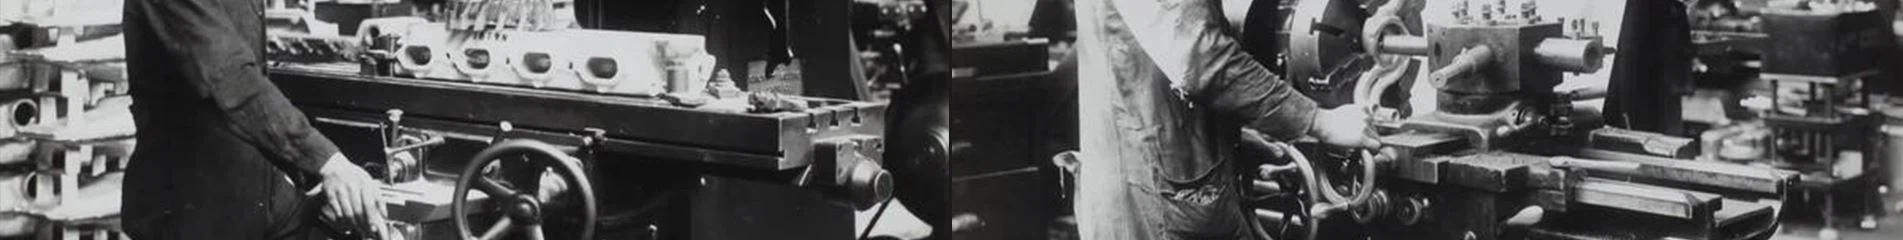
The car engines, aircraft parts, and mobile phone casings we see every day almost all rely on machining. Simply put, machining involves taking a raw metal blank and using various machine tools and cutters to remove excess material, shaping it into the specific dimensions and forms required by the blueprints.
An Overview of 7 Common Machining Methods - Zhihu
However, while they all involve cutting, methods such as turning, milling, planing, grinding, drilling, and boring differ significantly in their cutting techniques, the equipment used, and the types of tasks they can perform.
First, let's clarify a concept: machining precision.
Before discussing machining methods, we must understand the term "precision."
Precision refers to the difference between the dimensions of the finished part and those specified in the blueprint. The smaller the difference, the higher the precision. National standards classify precision into 20 grades, ranging from IT01 to IT18; a lower number indicates higher precision, while a higher number indicates lower precision.
Mechanical parts used in general factories typically have a precision of around IT7, whereas agricultural machinery parts are usually around IT8.
Another key indicator is surface roughness-essentially, how smooth or flat the part's surface is. It is measured in micrometers (μm); the lower the value, the smoother the surface.
I. Turning – Cutting while rotating
In turning, the workpiece rotates while the cutting tool remains stationary.
During the turning process, the workpiece is clamped onto the lathe's spindle and rotates at high speed, while the cutting tool moves linearly along the workpiece's surface, removing excess material layer by layer.
What is the lathe best suited for? Parts with rotational symmetry, such as shafts, discs, and sleeves. Simply put, almost anything shaped like a cylinder is produced on a lathe. Components like engine crankshafts and bearing races rely on turning.
CK61350 CNC Heavy-Duty Horizontal Lathe (Three-Guideway)_Dezhou Zhongtuo Machine Tool Manufacturing Co., Ltd.
Turning precision generally ranges from IT8 to IT7, with surface roughness between 1.6 and 0.8 micrometers. With precision turning, accuracy can be improved to IT6–IT5, and roughness reduced to 0.4–0.1 micrometers. When machining non-ferrous metals on a high-precision lathe using a diamond tool, the resulting surface can be as shiny as a mirror; this process is known as "mirror turning."
Lathes offer another advantage: the ability to perform various tasks simply by changing tools. By mounting an external turning tool, one can machine outer diameters; a boring bar allows for internal bore machining; and a threading tool enables thread cutting. A single standard horizontal lathe can handle a wide variety of machining operations.
II. Milling – Multi-cutter simultaneous cutting

In milling, the cutting tool rotates while the workpiece remains stationary or moves slowly.
Milling employs multi-toothed tools-specifically, milling cutters-where every tooth performs cutting as the tool spins. Due to the presence of multiple teeth and the absence of the "idle return stroke" found in planing, milling offers high efficiency.
What can milling machines do? They can machine flat surfaces, grooves, steps, gears, splines, threads, and complex mold surfaces-virtually anything. Consequently, milling is considered the most versatile machining process.
Mastercam Multi-axis Machining – Solutions and Techniques for Efficient Complex Surface Machining (Mastercam Chinese Website)
Milling typically achieves precision levels of IT8 to IT7 and surface roughness values between 6.3 and 1.6 micrometers. CNC milling machines offer higher precision, reaching the 0.01-millimeter level, while five-axis simultaneous CNC milling machines can achieve positioning accuracy of ±0.002 millimeters.
What is the main difference between turning and milling? Turning is suited for cylindrical and symmetrical parts, whereas milling is ideal for square, flat, or irregular parts with complex features. Generally, a shaft is turned, while a slotted square block is milled.
III. Drilling – Specialized for making holes
Drilling involves a rotating drill bit advancing into solid material to create a hole.
Drilling is the most fundamental method for hole making. It can be performed on dedicated drilling machines or on lathes, boring machines, and milling machines.
Z3050×16 Low-speed Heavy-duty Radial Drilling Machine – Tengzhou Gaodi Machine Tool Co., Ltd.
However, drilling has an inherent drawback: limited precision. Because drill bits are long and slender, they lack rigidity and tend to drift off-center during the operation. Drilling generally yields an accuracy of only IT13 to IT11, with a surface roughness of 50 to 12.5 micrometers. While some sources claim it can reach IT10, that is an optimistic estimate.
Consequently, a drilled hole is usually considered a rough-machined feature. If high precision is required, the hole must undergo further finishing processes such as counterboring or reaming.
IV. Boring – Refining the Hole
Boring involves machining an existing hole to make it larger, rounder, and smoother.
The tool used is called a boring bar (or boring tool); it is typically a single-point tool mounted on a bar that extends into the hole to perform the cutting.
The greatest advantage of boring is that the hole diameter is not strictly limited by the tool size. With drilling, the hole size is fixed by the drill bit diameter, whereas a boring tool allows for adjustable cutting depth within a certain range, offering much greater flexibility.
Boring can achieve an accuracy of IT9 to IT7 and a surface roughness of 2.5 to 0.16 micrometers. Precision boring can reach IT7 to IT6, with roughness levels between 0.63 and 0.08 micrometers.
A machining operation you may have heard of but never seen: boring-an eye-opening experience (Tencent Video).
The difference between drilling and boring is simple: drilling creates a new hole in solid material, while boring enlarges and refines an existing hole. One transforms "nothing into something," while the other transforms "rough into refined."
V. Planing – Back-and-Forth Scraping
Planing involves the tool moving back and forth in a straight line across the workpiece surface, much like a carpenter planing wood.
There are two main types of planers: the shaper (or reciprocating planer) and the gantry planer. Shapers are suitable for small to medium-sized workpieces, while gantry planers are designed for large workpieces.
Planing is primarily used to machine flat surfaces and straight slots. It is a common method for machining the guideways of large machine tools.
Gantry planer
Planing generally achieves an accuracy of IT9 to IT7 and a surface roughness of 6.3 to 1.6 micrometers. Rough planing is less precise (IT12 to IT11), whereas finish planing can achieve IT8 to IT7.
However, planing has a significant drawback: low efficiency. During the reciprocating motion of a planer, half the stroke is spent idling-performing no actual work. Consequently, in mass production, planing is increasingly being replaced by milling. Today, planing is primarily used for single-piece or small-batch production and for machining flat surfaces on large components.
VI. Grinding-Precision Achieved Through Abrasion
Grinding involves using an abrasive wheel to remove a thin layer of material from the workpiece surface.
Workpieces destined for grinding have usually undergone quenching (hardening) and possess high hardness; since standard turning or milling tools cannot cut them effectively, grinding wheels are required.
Grinding is a precision finishing process capable of achieving high accuracy-typically ranging from IT8 to IT5 or better-with surface roughness values between 1.25 and 0.16 micrometers. Precision grinding can reach 0.16 to 0.04 micrometers, ultra-precision grinding 0.04 to 0.01 micrometers, and mirror-finish grinding can achieve levels below 0.01 micrometers.
[Image]
Although grinding offers high precision, it is characterized by low efficiency and high costs. Therefore, it is usually the final step in the machining sequence; initial shaping is performed via turning, milling, or planing, leaving a small amount of material (allowance) for the final grinding pass.
Summary
Each of these six machining methods has its own specific application:
Turning: The primary method for rotary parts such as shafts, discs, and sleeves.
Milling: The most versatile method, used for flat surfaces, slots, gear teeth, and complex curved surfaces.
Drilling: Used to create new holes; the starting point for hole machining.
Boring: Used to enlarge and refine existing holes; offers much higher precision than drilling.
Planing: Used for flat surfaces and straight slots; low efficiency but suitable for large components.
Grinding: The final finishing step; used for high-hardness materials and achieves the highest precision.
Parts within a single machine often require a combination of these methods. For example, a shaft might first be turned to shape, then drilled, and finally have its outer diameter ground-proceeding step-by-step through rough machining, semi-finishing, and finishing.
With the advancement of CNC technology and intelligent manufacturing, these traditional machining methods are being redefined. Turn-mill machining centers can combine turning and milling operations into a single machine. Five-axis CNC machine tools allow for the machining of multiple surfaces in a single setup. AI technology can even enable machine tools to autonomously optimize machining paths, reducing reliance on the experience of veteran machinists. Machines are evolving, but the fundamental logic-determining which cutting method to use for a specific shape-will not change in the short term.


